Approve shade against a written light source and tolerance. Compare the lab dip with a finished bulk cutting and check dye-lot variation before approving shipment.
A buyer approves the fabric lab dip.
Bulk production starts.
Then the finished fabric arrives and somebody says:
“This is not the color we approved.”
This situation is familiar to many textile buyers, mills and garment manufacturers.
It can be frustrating because the color development stage appeared to be complete. The buyer selected a shade, approved the lab dip and expected bulk production to reproduce it exactly.
But textile color matching does not end when a lab dip is approved.
A lab dip is produced on a small scale under controlled laboratory conditions. Bulk fabric is dyed in a much larger production system and may later go through heat setting, washing, coating, calendaring, softening, DWR or other finishing processes.
The substrate itself may also vary between production lots.
All of these variables can affect the final shade.
This does not mean color variation should simply be accepted.
It means buyers and suppliers need a clear color approval system that defines:
- the approved color standard
- the agreed light source
- the acceptable shade tolerance
- the fabric stage at which color is approved
- how bulk dye lots are checked
- how shade variation within one dye lot is controlled
- how different rolls are grouped before shipment
At CC Textile, we treat lab dip approval and bulk shade approval as two related but separate stages.
The purpose is not to promise that textile color will never vary.
The purpose is to control that variation before the fabric reaches garment cutting.
What Does a Fabric Lab Dip Actually Approve?
A fabric lab dip is a small dyed sample prepared to show how a target color can be reproduced on a specific textile substrate.
In a typical development process, the buyer may provide:
- a Pantone reference
- a physical color standard
- an existing fabric swatch
- a garment reference
- another approved master sample
The dyeing laboratory then develops one or more color options.
These are usually submitted to the buyer for review.
The buyer may approve one option directly or request another round of correction.
Once one lab dip is approved, it becomes an important color reference for the next stage.
But what has actually been approved?
Normally, the buyer has approved the appearance of that particular dyed sample against the agreed color standard.
That approval does not automatically mean:
- every future dye lot will be visually identical
- every fabric construction will reproduce the color in exactly the same way
- the same recipe can be transferred to any fiber lot without adjustment
- finishing will have no effect on the final shade
- the color will look identical under every light source
- every roll in bulk production can be accepted without inspection
This distinction is important.
A lab dip is a color-development approval.
Bulk production still needs its own color control.
Buyers developing a new textile construction can also review our Fabric Development process, where color development is considered together with the fabric structure and intended finishing route.
Why a Lab Dip and Bulk Dye Lot Can Look Different
A laboratory sample and a production dye lot are not produced under identical conditions.
The scale is different.
The equipment is different.
The amount of fabric is different.
The process control requirements are also different.
A lab dip may involve only a very small quantity of fabric.
Bulk dyeing may involve hundreds or thousands of meters in one production lot.
When the process moves from the laboratory to bulk production, several variables can affect the final shade.
Dyeing scale
A laboratory recipe must be translated into a production-scale process.
Temperature, time, liquor movement, chemical addition and dye absorption need to be controlled across a much larger quantity of material.
The objective is to reproduce the approved shade as closely and consistently as possible.
However, textile dyeing is a production process, not digital color printing from a computer screen.
Process variation must therefore be monitored.
Fabric substrate
The color result is influenced by the material being dyed.
If the base fabric changes, the final shade can also change.
Relevant differences may include:
- fiber composition
- yarn lot
- yarn lustre
- filament structure
- fabric density
- weave
- pretreatment
- optical appearance of the undyed fabric
Two fabrics can receive a similar dye formulation but still reflect light differently.
That can make the final colors appear different even when the dyeing process itself is well controlled.
Fiber and yarn lot variation
Different raw-material lots may not behave exactly the same during dyeing.
This is one reason color-critical programs should control raw-material lots whenever practical.
If a garment program requires several production batches over a long period, buyers should not automatically assume that a lab dip developed on one substrate can be reproduced indefinitely without adjustment.
The production fabric still needs to be checked.
Process conditions
Changes in dyeing conditions can influence shade depth and tone.
The effect depends on the fiber system, dyestuff and production method.
This is why bulk dyeing should follow controlled production parameters and should not rely only on the fact that a lab dip was previously approved.
Fabric Construction and Finishing Can Shift the Shade
Color is not only influenced by dye.
Fabric construction and finishing can also change how a color looks.
This is particularly important for outdoor woven fabrics because many of them go through several finishing stages after dyeing.
Fabric density and surface
A dense plain weave, ripstop or twill can reflect light differently.
The yarn shape, filament structure and surface texture can affect the visual depth of the color.
A smooth, compact surface may appear different from a more textured surface even when the underlying color is close.
This is why approving a color on one construction and automatically transferring it to another fabric can create problems.
Heat setting
Heat setting can affect the appearance of synthetic fabrics.
The degree of change depends on the fiber, color and production conditions.
If the approved lab dip and the bulk fabric have not passed through comparable processing stages, the visual comparison may not be meaningful.
Calendaring
Calendaring changes the fabric surface.
It can make the surface smoother, flatter or more lustrous.
That change in light reflection can make a shade appear darker, lighter or simply different to the eye.
The dye itself may not have changed significantly, but the way the finished surface reflects light has changed.
Softening and other chemical finishes
Softening agents and other finishing treatments may also influence the visual appearance of some colors.
The effect may be small, but color-sensitive projects should still evaluate the fabric after the intended finishing process.
DWR, coating and lamination
Outdoor fabrics may also receive:
- DWR finishing
- PU coating
- TPU membrane lamination
- backing fabric lamination
- other functional finishes
Some of these processes mainly affect the reverse side of the fabric, while others can influence the face appearance as well.
For this reason, buyers should define whether color approval refers to:
- dyed fabric before finishing
- finished face fabric
- coated fabric
- laminated fabric
The production stage matters.
A color approved before finishing should not automatically be treated as final approval if the subsequent process changes the appearance.
Why Color Must Be Checked Under Agreed Light Sources
One of the most common causes of color disputes is simple:
The buyer and supplier are not looking at the fabric under the same light.
A shade may look acceptable under one light source and noticeably different under another.
This can happen because different light sources have different spectral characteristics.
A related issue is metamerism.
Two color samples may appear very similar under one light source but show a noticeable difference under another.
For textile color approval, saying:
“Please match the Pantone color”
is therefore not always enough.
The buyer should also define how the color will be evaluated.
Depending on the customer’s color program, the agreed light sources may include recognised daylight, retail or artificial-light conditions.
The exact requirement should come from the buyer’s specification.
CC Textile does not assume that one lighting condition is correct for every customer.
If the brand has an established color approval standard, we follow that requirement.
The same principle applies to instrumental color measurement.
If the buyer uses spectrophotometer data or a specified color-difference tolerance, the method and acceptance criteria should be agreed before bulk approval.
A numerical color difference should not be invented after the fabric has already been produced.
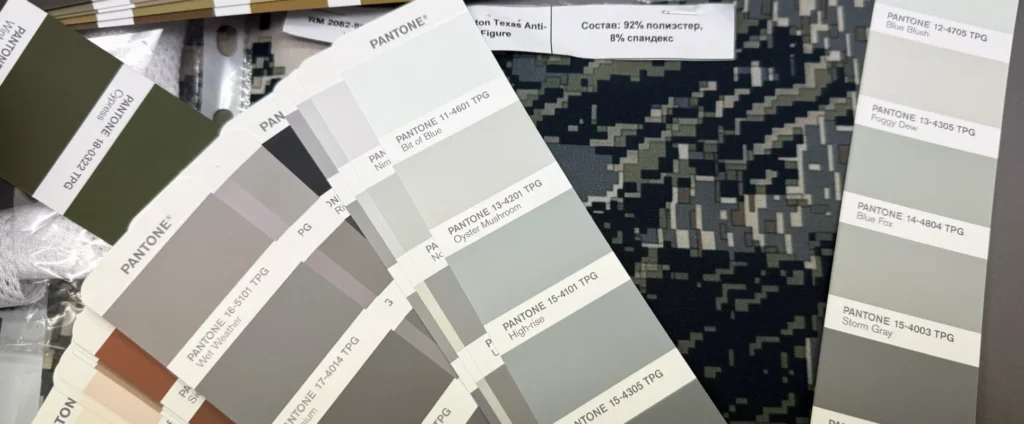
Pantone is a target, but the textile sample still matters
Pantone references are widely used when communicating target colors.
They are very useful.
But a printed Pantone reference and a dyed textile surface are not physically identical materials.
A textile has:
- fibers
- yarn texture
- weave
- lustre
- surface irregularity
- directional reflection
These characteristics influence how color is perceived.
For this reason, once a fabric lab dip has been approved, the approved textile sample usually becomes a more practical production reference than repeatedly comparing bulk fabric only with a printed color chip.
The original target still matters, but the approved fabric standard becomes extremely important for bulk control.
Lab Dip Approval vs Bulk Shade Approval
This is one of the most important distinctions for buyers.
Lab dip approval is not the same as bulk shade approval.
The lab dip establishes the target shade on the chosen fabric.
Bulk shade approval confirms whether the actual production lot is acceptable against that approved standard.
A good color-control process therefore has at least two checkpoints.
Stage 1: Lab dip approval
The buyer reviews the color-development samples and approves the preferred shade.
That approved sample should be identified and retained as a controlled reference.
Stage 2: Bulk shade approval
Once bulk dyeing has been completed, representative cuttings from the production fabric are compared with the approved standard.
The comparison should follow the agreed lighting and color-evaluation requirements.
If the bulk shade is acceptable, the lot can move forward.
If it is outside the agreed range, the supplier and buyer need to decide the appropriate corrective action before shipment.
The important point is that approval should happen before a color issue becomes a garment-production problem.
At CC Textile, bulk color control is part of the wider production and inspection process described in Quality & Compliance.
How Buyers Should Handle Shade Bands and Roll Grouping
Even when the overall dye lot is acceptable, buyers may still need to consider variation within or between rolls.
This is where shade bands and roll grouping become useful.
What is a shade band?
A shade band is a controlled set of actual production fabric cuttings used to represent the acceptable shade range or the shade variation found within a bulk lot.
The exact procedure depends on the customer’s quality system.
The purpose is to make shade evaluation more practical.
Instead of describing a difference only as:
“slightly darker”
or:
“a little more blue”,
the buyer and supplier can work with actual physical examples.
Dye lot variation
If a color requires more than one dye lot, each lot should be evaluated.
Two dye lots may both fall within the buyer’s acceptable range while still not being visually identical to each other.
That difference becomes important during garment cutting.
Head, middle and tail shade
Color should not always be checked from only one position.
Depending on the production method and fabric, buyers may require shade checking from different parts of the lot or roll, including:
- head
- middle
- tail
This helps identify shade variation along the length of the fabric.
If only one small cutting is checked, an internal variation may be missed.
Roll-to-roll variation
Different rolls should also be compared where required.
If the color variation is visible, rolls can be grouped into similar shade families.
This is particularly important before garment cutting.
A garment factory should avoid mixing visibly different shade groups within the same garment or matched garment set.
For example, using one shade group for a jacket body and a noticeably different shade group for sleeves may create an obvious panel mismatch.
Roll grouping helps the garment factory manage this risk.
Keep shade identification through the supply chain
If rolls have been grouped by shade, that information should not disappear when the fabric reaches the garment factory.
Roll identification and shade grouping need to remain traceable.
Otherwise, good color control at the fabric stage can be lost during spreading and cutting.
Color control therefore involves both the fabric supplier and the garment manufacturer.
Bulk Color Approval Checklist
Before placing a color-sensitive fabric order, buyers can reduce risk by defining the approval process in advance.
1. Confirm the color target
Provide a clear reference.
This may be:
- Pantone reference
- physical color standard
- approved garment
- approved fabric swatch
- brand master standard
Avoid relying only on a color displayed on a phone or computer screen.
2. Confirm the exact fabric construction
Color approval should be made on the intended substrate whenever possible.
Changes in fiber, yarn, weave or surface can change the appearance.
3. Approve and retain the lab dip
Once a lab dip is approved, identify it clearly.
Both buyer and supplier should work from the same approved reference.
Avoid situations where different departments are using different versions of the color standard.
4. Define the light source
Specify the lighting conditions used for color approval.
This is especially important if the brand has strict retail or metamerism requirements.
5. Define the color tolerance
If the buyer uses visual limits, shade bands or instrumental tolerances, these should be agreed before bulk production.
Do not wait until shipment to decide what color difference is acceptable.
6. Define the approval stage
Confirm whether the color is approved:
- after dyeing
- after finishing
- after coating
- after lamination
For most finished-fabric purchases, the buyer needs to know how the final commercial fabric looks.
7. Check the first bulk dye lot
Do not assume lab dip approval replaces bulk approval.
Representative bulk cuttings should be checked against the approved standard.
8. Check head, middle and tail where required
For color-sensitive orders, evaluate whether there is shade variation within the production length.
9. Check different dye lots separately
If the total order requires multiple lots, do not assume the first approved lot automatically represents all later lots.
10. Group rolls where necessary
If acceptable but visible shade differences exist, group similar rolls together.
Provide the grouping information to the garment factory.
11. Keep records
Retain the approved lab dip, bulk approval sample, dye lot information and relevant inspection records.
These references become especially valuable if the color is reordered later.
A Lab Dip Is the Beginning of Bulk Color Control, Not the End
An approved fabric lab dip is important.
Without it, the dyeing mill does not have a properly approved color target.
But lab dip approval should not be confused with final bulk fabric approval.
Between the laboratory and the finished production fabric, several variables can change the way a shade looks:
substrate + fiber lot + dyeing conditions + fabric construction + finishing + light source + production lot
The objective is therefore not to assume that every bulk meter will be visually identical to a small laboratory sample.
The objective is to establish a color-control system that identifies unacceptable variation before the fabric is shipped or cut into garments.
For buyers, the most useful specification is not simply:
“Match Pantone XXXX.”
A stronger specification defines:
the color standard + approved lab dip + evaluation light source + tolerance + finished-fabric stage + bulk approval method + shade control requirements.
That gives both buyer and supplier a much clearer basis for production.
It also reduces the risk of discovering a color problem only after thousands of meters have already been produced.
If you are developing a woven fabric and need to control color together with construction, finishing or performance requirements, you can review our Fabric Development process or contact CC Textile with your specification and color reference.
Color control is also connected with commercial decisions. Different fibers, dyeing processes, finishes and production requirements can affect manufacturing cost, which we discuss further in Why Fabric Prices Vary.
For an additional textile industry resource covering sourcing and technical discussions, buyers can also visit Tex-Alliance.
You can also follow CC Textile on Facebook for updates on fabric development, production and textile quality control.
Frequently asked questions
What is a lab dip in textiles?
A fabric lab dip is a small dyed textile sample prepared to match a target color before bulk production. Once approved, it becomes an important color reference, but the finished bulk dye lot still needs separate shade control and approval.
Why can bulk fabric look different from the approved lab dip?
Bulk shade can be affected by production scale, fabric substrate, fiber and yarn lots, dyeing conditions, heat setting, calendaring and other finishing processes. This is why an approved lab dip does not replace bulk shade inspection.
Should fabric color be checked under a specific light source?
Yes. Fabric shades can appear different under different light sources, and metamerism may cause two samples to match under one light but not another. Buyers should define the required light source and color approval conditions before bulk production.
What is the difference between lab dip approval and bulk shade approval?
Lab dip approval confirms the selected color during development. Bulk shade approval confirms whether the actual production fabric is acceptable against that approved standard after the required production and finishing processes.